ENGINEERED AROUND YOUR PROCESS
Robotic Welding
The weld process, the fixture, and the robot developed together around your part. Because the robot is rarely the hard part.
Discuss your application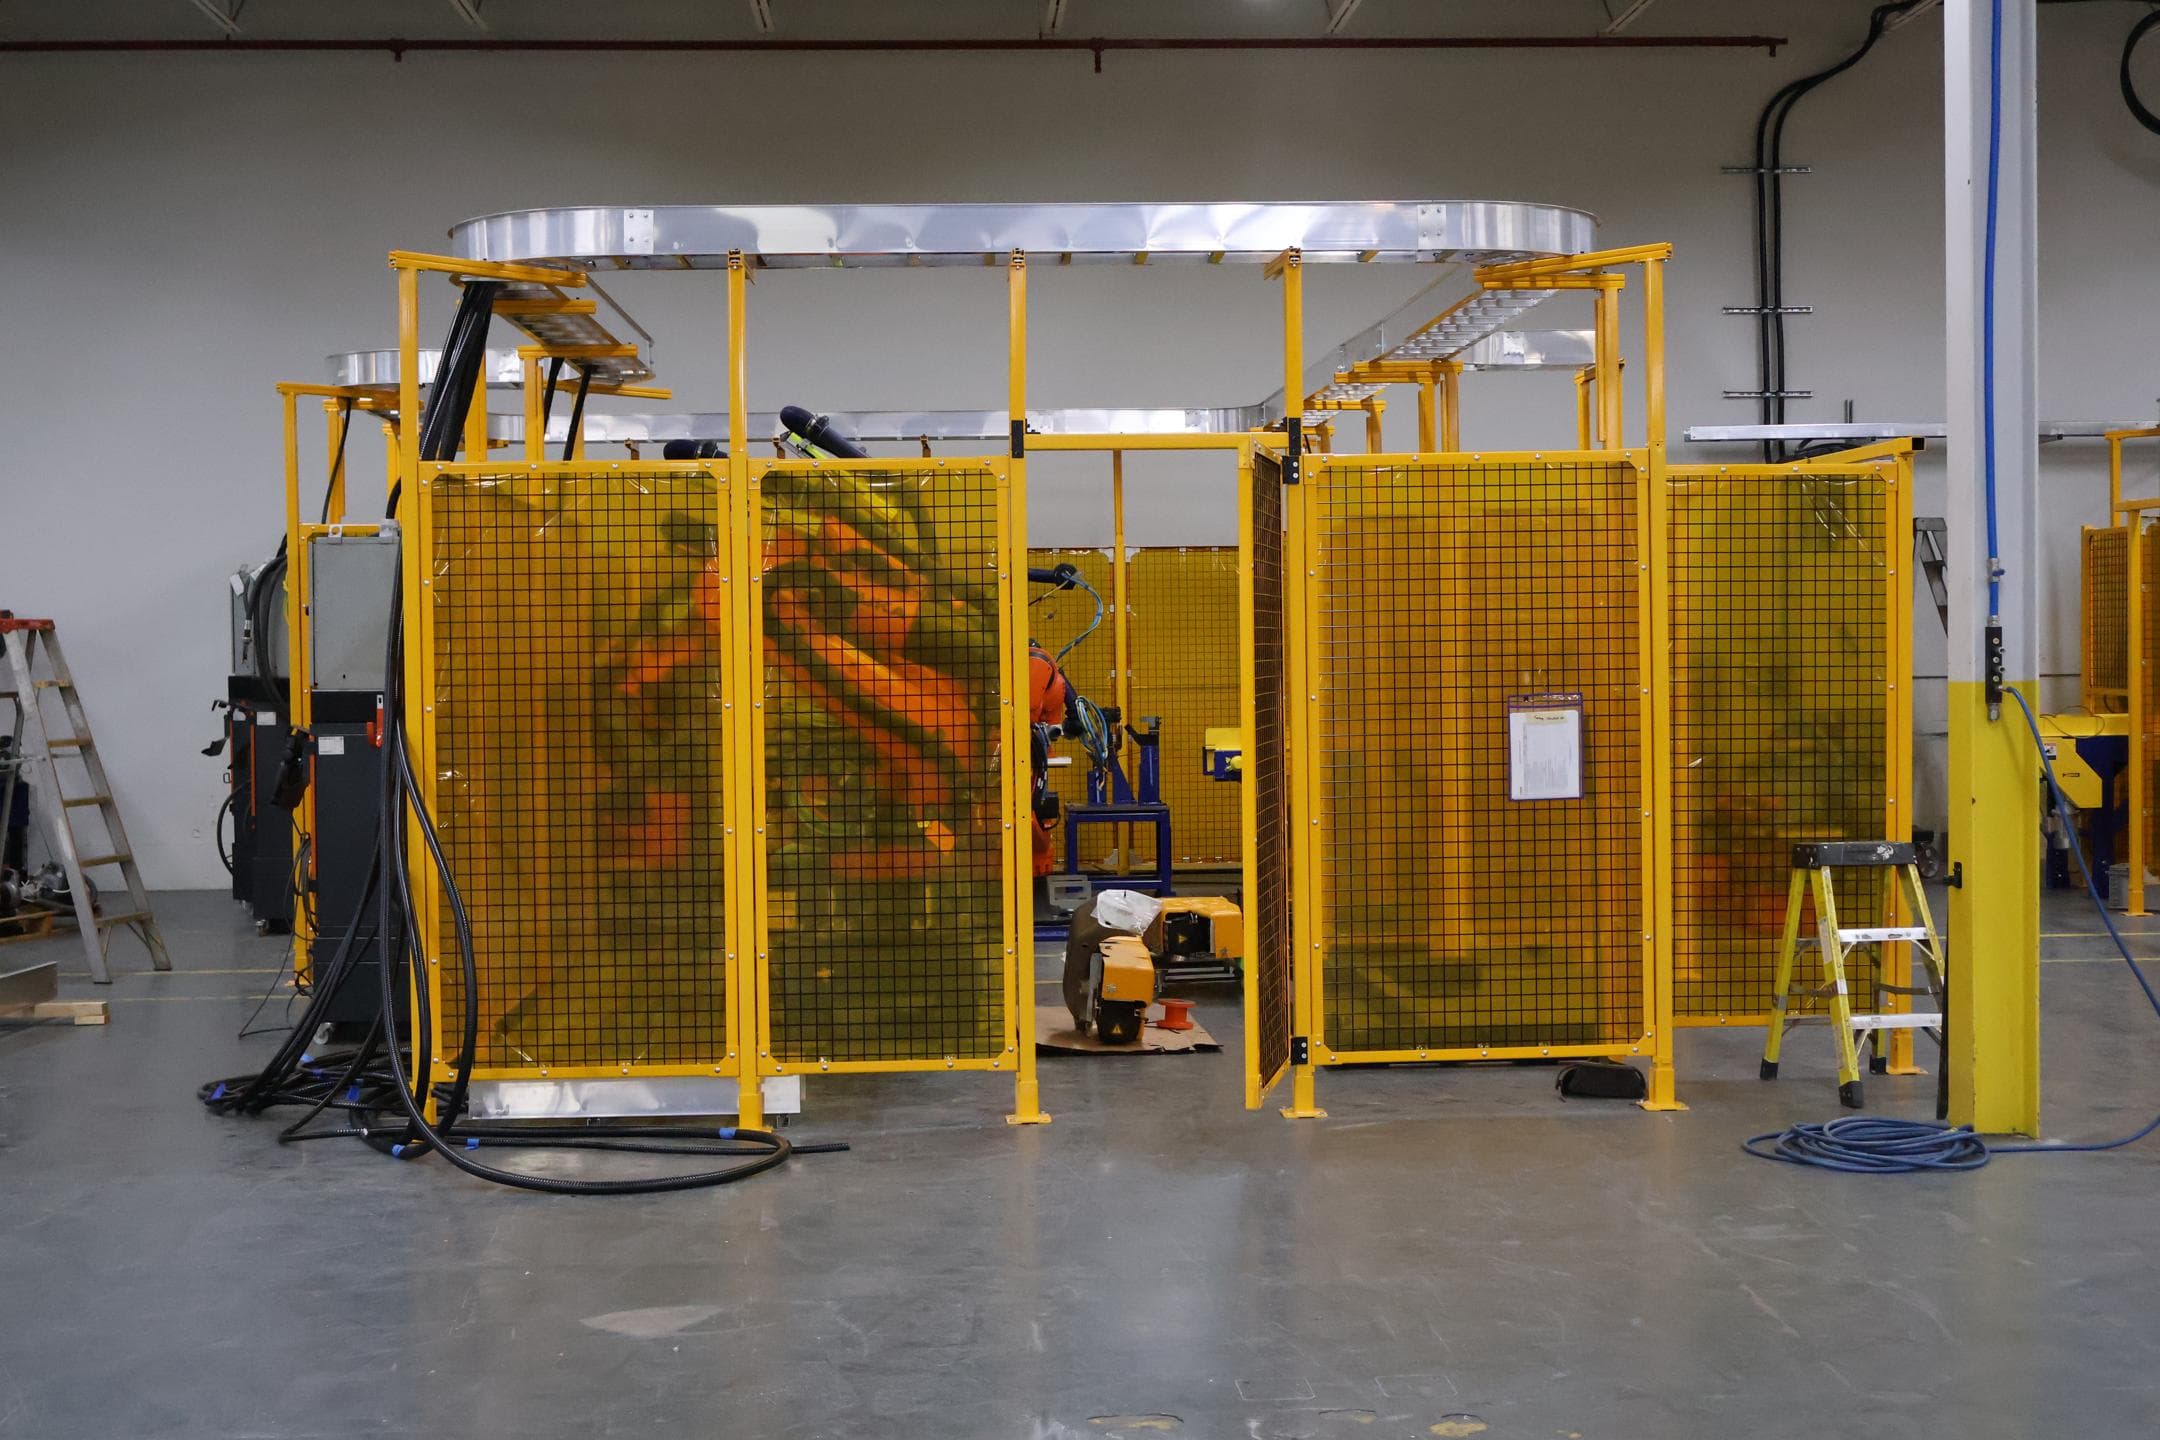
The problem this solves
Three things usually bring people to robotic welding, and they are not the same problem.
- You cannot find welders.
- Skilled welders are hard to hire and harder to keep, and the ones you have are doing work that does not need their skill. This is a capacity problem with a labour cause, and it is the most common reason a first robotic weld cell gets funded.
- Your welds are inconsistent.
- Not bad, but variable. Rework moves with who is on shift. A dimension drifts and nobody can point to when. This is a quality problem, and robots solve it more completely than they solve the first one.
- The weld has to happen somewhere a person should not be standing.
- Fume, confined access, awkward position. This comes up less and matters more. For low volumes that would never justify automation on cycle time alone, that can still be the right call.
What we actually do
What all three have in common is that the answer is not “buy a welding robot.” A robot repeats what you give it. If the process is not right, or the part does not land in the same place every time, the robot will repeat the problem faster and more consistently than a person did.
- Develop the weld process first.
- Parameters, sequence, and heat management for your material, thickness, and joint. Proven on your parts before anything is designed around it.
- MIG, TIG, spot, and projection.
- Matched to the joint and the production requirement, not to what we happen to own.
- Fixturing and tooling.
- Locating, clamping, and holding the part through the weld, including managing the distortion the heat introduces. Fixture design is where most weld cells are actually decided.
- Positioners and part manipulation.
- Presenting the joint to the torch at the right angle rather than asking the robot to reach an awkward position it will reach badly.
- Seventh-axis track where it earns its place.
- A robot is typically bolted down with six axes. Adding a linear track gives it reach that would otherwise need a longer and more expensive arm, lets one robot work several stations along a line, and often removes the need for a second robot entirely. On a weld cell that can be the difference between one robot and two.
- Weld monitoring and inspection.
- Flagging the conditions that cause a quality issue so downtime and rework get caught early rather than at final inspection.
- Full cell integration.
- Load, weld, inspect, unload, as one sequence under one control system.
What robotic welding is actually good at
Worth being straight about, because the honest answer sells better than the brochure one.
- Accuracy.
- Where a weld needs precision, a robot holds it. Even at lower volumes, accuracy requirements alone can justify the cell through reduced rework.
- Repeatability.
- The more repeatable the joint, the faster a robot pays for itself. This is the single best predictor of whether your part is a good candidate.
- Safety.
- Dull, dirty, and dangerous work is where robots belong. If the atmosphere is hazardous, that can outweigh the volume maths.
- Consistency over time.
- Once proven, quality stays where you put it. Third shift welds like first shift.
- Where it is a poor fit:
- very low volume with high part variety and no repeatable fixturing strategy. If every part is different and locating them is manual, you are automating the wrong step. We will tell you that rather than sell you a cell.
Starting a conversation
- The part, the joint, and the material. Thickness, joint configuration, and the weld specification if there is one.
- Volume and variant count. How many, how many versions, and how often they change.
- What is driving it. Labour, quality, safety, or capacity. The driver changes the right answer.
If the weld process itself is not established yet, that is Process Development & R&D, and it is the right place to start rather than a detour.
PROVEN ON THE PRODUCTION FLOOR
All case studiesNine Years of Almost
Rebuilding a BEV rear axle line out of its own parts
7–9 yearsThe previous line ran without ever meeting quality or cycle timeRead the project AutomotiveNine Seconds a Part
Six variants through one reused cell, with no changeover
9 sA completed assembly out of the cell, welded, inspected, marked and packedRead the projectRELATED CAPABILITIES
Process Development & R&D
Resolve the difficult picks, delicate parts, and process unknowns through focused trials and prototype tooling.
Read moreMachine Design & Tooling
Turn a production requirement into practical machine layouts, custom fixtures, and end-of-arm tooling.
Read moreRobotic Systems & Assembly
Connect part handling, assembly, inspection, and packaging in a complete robotic cell or production line.
Read moreTHE NEXT MOVE IS YOURS.
What could we
build together?
Bring your part, your process, or the problem you haven’t solved yet.
Download the capability sheet One page. No form.